News & Events
Air Knife Drying on Bakery Lines: Where the Pressure Window Sits
Reliable surface drying depends on momentum, mounting distance and exposure time—not heat alone.
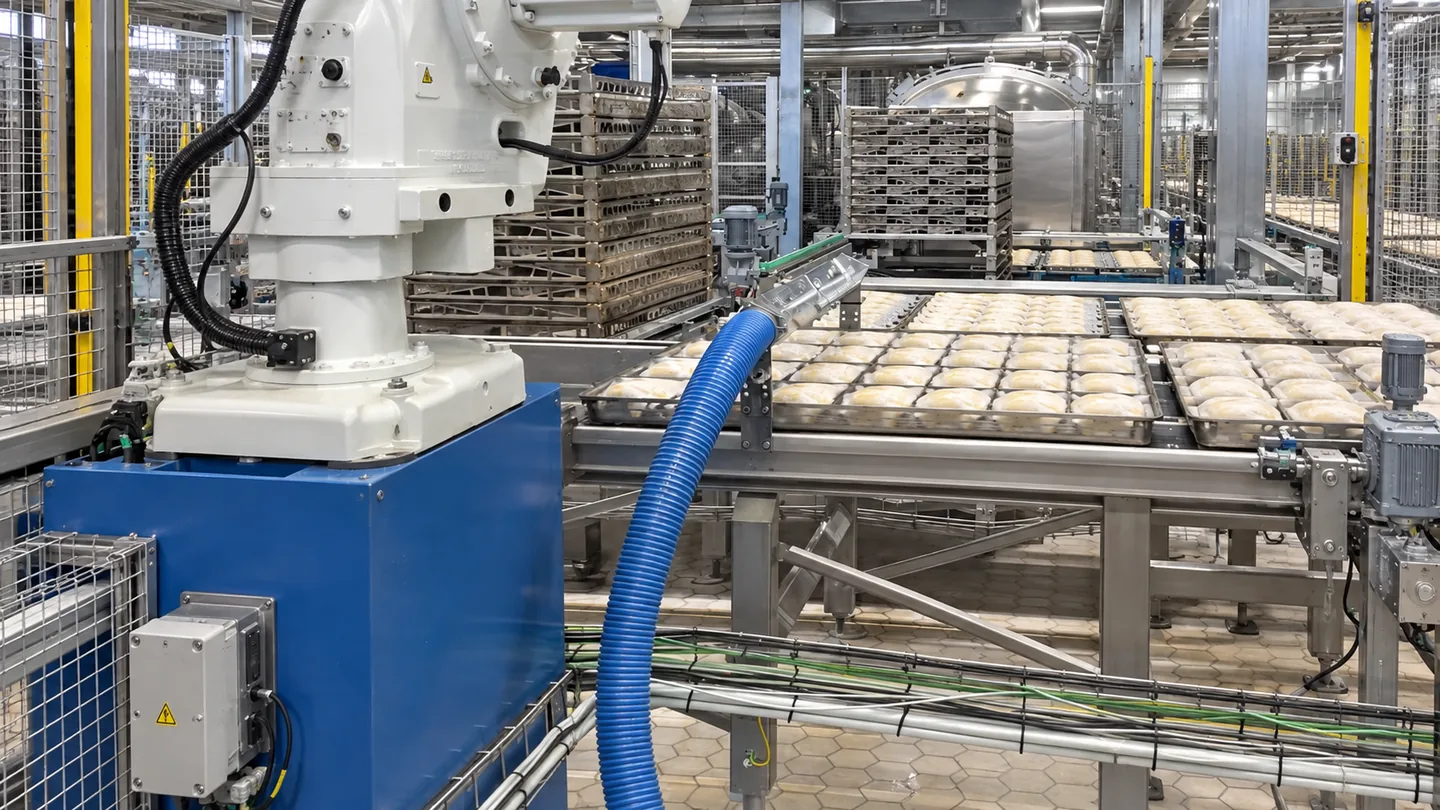
Packaged bakery products leave the wrapping section with moisture and crumbs on the film surface. Downstream operations do not tolerate it.
Moisture on a package is rarely an aesthetic problem. Corrugated cases lose compression strength as board moisture rises. A wet film blocks label adhesion and ink bonding, while water in the seal area weakens the seal. The cost of a wet package appears three stations later.
Removing it is a momentum task, not a thermal one. On a 500 ml container with a 20 micron water film, evaporation removes only a small share of the water in the available exposure time. The rest has to be stripped mechanically by a high-velocity air curtain.
Droplets near 0.5 mm release at roughly 30 m/s impingement velocity. The smaller droplets and thin films that remain on a package surface need 60 to 80 m/s. Allowing for jet decay, this maps to a pressure rise of 15 to 20 kPa. Above roughly 25 kPa, the return falls away.
The GALEX X720 high-speed turbo blower is built for this band. Its 7.5 kW drive covers the pressure rise and air volume needed by an air knife spanning a standard conveyor width.
Mounting distance and exposure time decide the result. Moving a knife from 20 mm to 50 mm from the product cuts impingement velocity by about a third. At 1.5 m/s line speed, a second knife in series doubles exposure and can improve results more effectively than raising pressure.
For continuous blow-off, blower-driven knives replace compressed air at a fraction of the energy, making them particularly effective on lines running several shifts.